


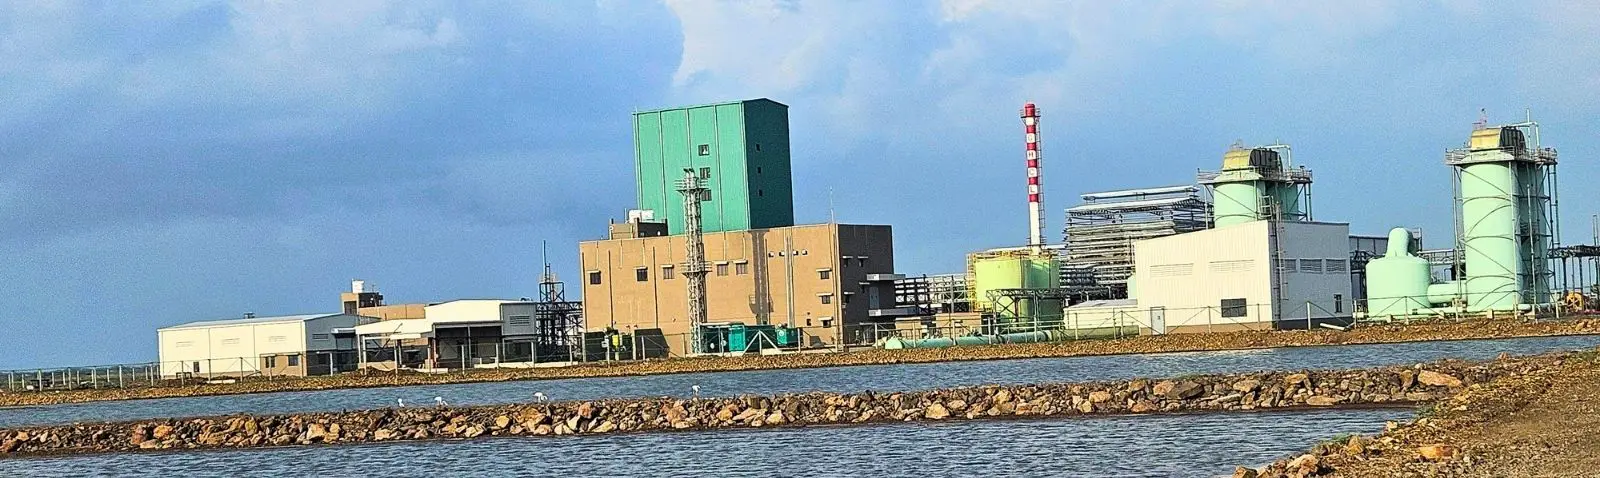
In 2026, GHCL marked an important milestone in its diversification journey with the commencement of commercial production of liquid Bromine and Vacuum Salt, strengthening its presence across new product segments.
In 2026, GHCL marked an important milestone in its diversification journey with the commencement of commercial production of liquid Bromine and Vacuum Salt, strengthening its presence across new product segments.
GHCL commenced commercial production of liquid Bromine on October 12, 2026, marking a significant step in expanding its product portfolio beyond its existing offerings. The new facility, located at the company’s plant in Kathivadar, Rajula, Amreli district, Gujarat, has an annual production capacity of 2,800 MT.
As an addition to GHCL’s growing portfolio, Bromine strengthens the company’s presence in the chemicals and commodity chemicals segment. The facility is designed to cater to both domestic and international markets, enabling GHCL to serve customers across multiple geographies.
The commencement of Bromine production reflects GHCL’s continued focus on diversification, building on its manufacturing capabilities to address evolving market requirements. With the new facility operational, the company is positioned to expand its customer reach and develop opportunities across a wider market.
Through this expansion, GHCL continues to build on its established manufacturing strengths while broadening its product basket and creating new avenues for growth. The addition of Bromine marks another step in the company’s journey towards a more diversified portfolio.
GHCL marked a significant milestone in its diversification journey with the commencement of Vacuum Salt production under its brand, Na Salt. Strategically integrated within GHCL’s Soda Ash facility, the plant is located at Sutrapada, in the Gir Somnath district of Gujarat. With an annual production capacity of 0.22 MMTPA, the facility combines manufacturing efficiency with a focus on product quality.
Vacuum salt is known for its high purity, uniform crystal size and consistent quality, making it suitable for food, pharmaceutical and industrial applications. Its controlled production process supports consistency and hygiene, meeting the requirements of applications where these attributes matter.
A key feature of the facility is its use of waste heat generated during soda ash manufacturing through the Solvay process to evaporate salt. By eliminating the need for additional energy and productively repurposing available process heat, we establish a high cost-efficient, low-cost manufacturing process, reflecting GHCL’s commitment to sustainable innovation.
The plant also stands out for its all-women workforce, with women managing critical operations, underscoring GHCL’s vision for a diverse workplace.
 Toll Free: 1800 2700 445